Explore our industrial-grade, biocidal-infused flooring substrates designed for high-sanitation environments, pharmaceutical facilities, data centers, and eco-conscious architectural projects.


In a post-pandemic industrial landscape, the global demand for surface protection has transitioned from reactive chemical disinfection to proactive, permanent bio-passivation. Anti-microbial surface coatings have become integral components of modern infrastructure, architectural surface design, medical manufacturing, and cleanroom technologies.
Engineered via advanced inorganic carrier synthesis (such as silver-ion zeolites, copper micro-composites, and titanium dioxide photocatalysts) as well as organo-silane quaternary ammonium compounds, these coatings actively suppress the proliferation of human pathogens, hospital-acquired infections (HAIs), mold spores, and biofilm networks without leaching harmful volatile organic compounds (VOCs).
Antimicrobial surface coatings operate through continuous chemical and physical biocidal mechanisms. Unlike sacrificial surface disinfectants that evaporate within minutes, embedded antimicrobial coatings create an uninhabitable surface micro-environment for micro-organisms.
Silver-ion technology remains the gold standard for solid surfaces, medical-grade flooring, cleanroom paneling, and WPC/SPC co-extruded architectural products. Silver ions are encapsulated within inert ceramic micro-carriers (zeolites or glass matrices). When moisture interacts with the surface, silver ions are released at controlled parts-per-million (ppm) levels. These ions bind to bacterial cell wall proteins, rupture cell membranes, inhibit cellular respiration, and interrupt DNA replication cycles, delivering a 99.99% log-4 reduction in pathogen density.
Utilizing ambient light energy, nano-scale titanium dioxide coatings produce reactive oxygen species (ROS) such as hydroxyl radicals (.OH) and superoxide anions (.O2-). These ultra-reactive molecules instantly oxidize organic contaminants, cellular membranes, and airborne virus particles on surface contact, rendering surfaces self-cleaning and odor-neutralizing.
Providing physical, non-leaching lysis, quaternary ammonium silanes bond covalently to organic and inorganic substrates. They form a micro-layer of positively charged molecular "spikes." Negatively charged bacterial membranes are physically attracted to these spikes, causing mechanical cell puncture and lysis without promoting antibiotic resistance mutation.
Based on manufacturing capacity, R&D patents, ISO compliance, global export volume, and material synthesis capability, the following top 10 manufacturers lead the global market:
| Manufacturer / Brand | Core Technology Matrix | Primary Export Markets | Key Industry Focus |
|---|---|---|---|
| Anhui Prairie Floor Co., Ltd. | Co-extruded Ag+ Polymer, Anti-static Polyurethane, Low-VOC WPC/SPC | North America, Europe, SE Asia, Middle East | Cleanrooms, Healthcare, Commercial Flooring, Sustainable Outdoor WPC |
| AkzoNobel N.V. | Interpon AM Powder Coatings, Bio-based Synthetic Polymers | Global (Europe, Americas, APAC) | Architectural Powder Coating, Industrial Metals |
| PPG Industries, Inc. | SILVERSHIELD™ Technology, Copper-infused Marine Coatings | Global | Aerospace, Healthcare Facilities, Industrial Equipment |
| The Sherwin-Williams Company | PaintShield® Microbicidal Paint, Polyaspartic Resins | North America, South America, Europe | Hospitals, Educational Institutions, High-Traffic Commercial |
| Microban International | Custom Antimicrobial Additive Synthetics, Zinc Pyrithione | Global Export & Licensing | Polymer Additives, Synthetic Flooring, Textiles |
| BioCote Ltd. | Silver Ion Technology Integration, Additive Concentrates | Europe, North America, Asia | Contract Manufacturing, Flooring Compounds, Consumer Goods |
| Lonza Group (Arxada) | Omacide™ Biocides, Quaternary Ammonium Compounds | Global | Raw Material Biocides, Specialty Chemical Formulations |
| Nippon Paint Holdings | Anti-Viral Photocatalytic TiO2, Eco-Clean Waterborne Coatings | APAC, Middle East, Europe | Commercial Infrastructure, Healthcare Surfaces, Residential |
| BASF SE | Bactronix Hydrophobic Additives, Polyurethane Dispersion | Global | Industrial Resin Coatings, Automotive, Construction Chemicals |
| Kansai Paint Co., Ltd. | Shikkui Calcium Carbonate Anti-Viral Coatings | Asia, Africa, Europe | Air-Purifying Interior Surfaces, Public Infrastructure |
China has solidified its position as the global hub for advanced material synthesis, co-extrusion technology, and eco-friendly antimicrobial surface flooring production. Overseas buyers, B2B importers, and enterprise contractors leverage specific strategic manufacturing advantages when sourcing from top-tier Chinese producers:
Leading Chinese manufacturing ecosystems combine raw material refining (PVC, WPC resin, bio-cork, specialty epoxy polymers) with active biocide masterbatch synthesis. By directly compounding antimicrobial silver-zeolite additives into structural polymer cores during extrusion, factory-direct operations eliminate intermediary markups and guarantee uniform chemical dispersion throughout the product substrate.
China's modern production facilities utilize multi-layer co-extrusion machinery. Unlike standard top-coat spray applications that wear away under foot traffic or heavy machinery, co-extruded antimicrobial WPC and SPC products feature a wear layer fused permanently to the core. This extends surface service life by over 50% while preserving active antibacterial efficacy under intense friction.
Modern Chinese manufacturers operate under rigid national environmental mandates (GB/T standards) alongside international certifications including ISO 9001, ISO 14001, FloorScore®, CE, and REACH. Advanced UV tempering lines ensure near-zero volatile organic compound emissions, meeting strict indoor air quality (IAQ) criteria for healthcare and cleanroom installations.
From custom color palettes and specialized acoustic underlayments to tailored static-dissipative resistance values ($10^6$ to $10^9$ ohms), Chinese high-volume manufacturing lines deliver rapid prototyping, continuous quality control, and flexible minimum order quantities (MOQs) tailored for large-scale commercial contracts.
Anhui Prairie Floor Co., Ltd. is a globally recognized brand and leader in the field of WPC (Wood Plastic Composite), SPC, elevated cleanroom floor panels, and advanced surface-treated building materials. Since our establishment, we have focused on transforming recycled resources into high-quality plastic wood products and specialized functional flooring, reducing dependency on natural forests and promoting sustainable development for the planet.
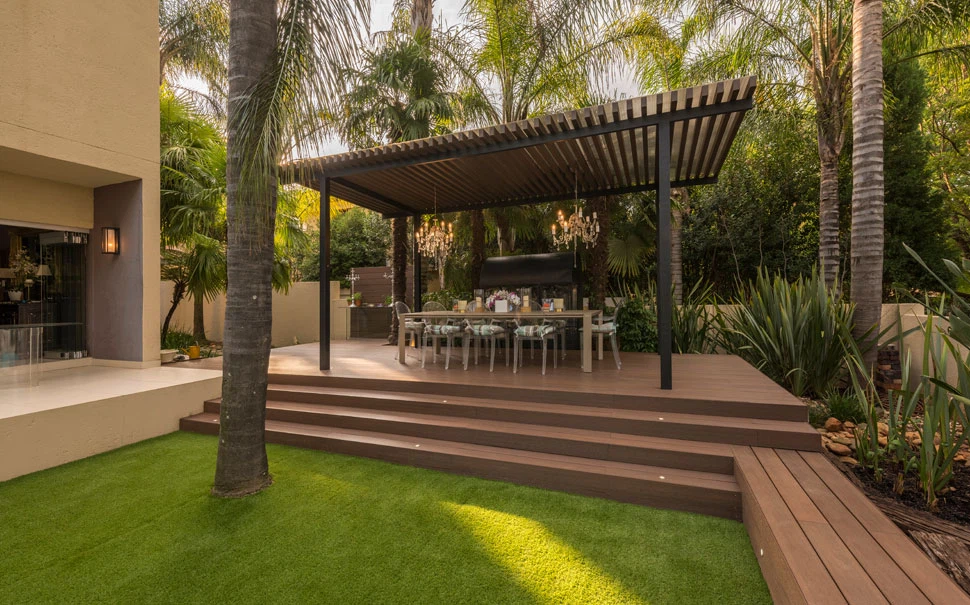
We started with a simple belief: to provide everyone with a beautiful, low-maintenance outdoor space. At Anhui Prairie Floor, we are committed to offering eco-friendly and aesthetically pleasing flooring solutions for patios, gardens, terraces, industrial cleanrooms, and high-tech facilities. Our mission is to deliver products that not only serve a functional purpose but also enhance people's well-being while caring for the environment.
Vision: "To become the world's leading brand of sustainable outdoor construction materials and antimicrobial indoor functional floors, reshaping the connection between people and nature through technological innovation."
We apply co-extrusion technology to our WPC and SPC products, ensuring greater wear resistance on the surface layer, higher toughness in the internal composite core, and an extended service life by 50%. This ensures that our floors maintain structural integrity and antimicrobial activity under tough conditions.
From raw material verification to continuous automated extrusions, our manufacturing processes undergo strict quality control protocols meeting international benchmarks such as ISO 9001 and ISO 14001.
We offer a comprehensive selection of finishes, embossed textures, anti-static ratings, and color palettes. Our flooring lines are available in seven standard colors with rapid custom matching for bespoke architectural projects.
We deliver an end-to-end service experience encompassing CAD layout optimization, structural load estimation, custom OEM formulation, and global shipping logistics.
Our modern multi-line WPC, SPC, and polyurethane coating extrusion lines guarantee stable output, empowering us to service mega-scale commercial projects and worldwide export distributors without delay.
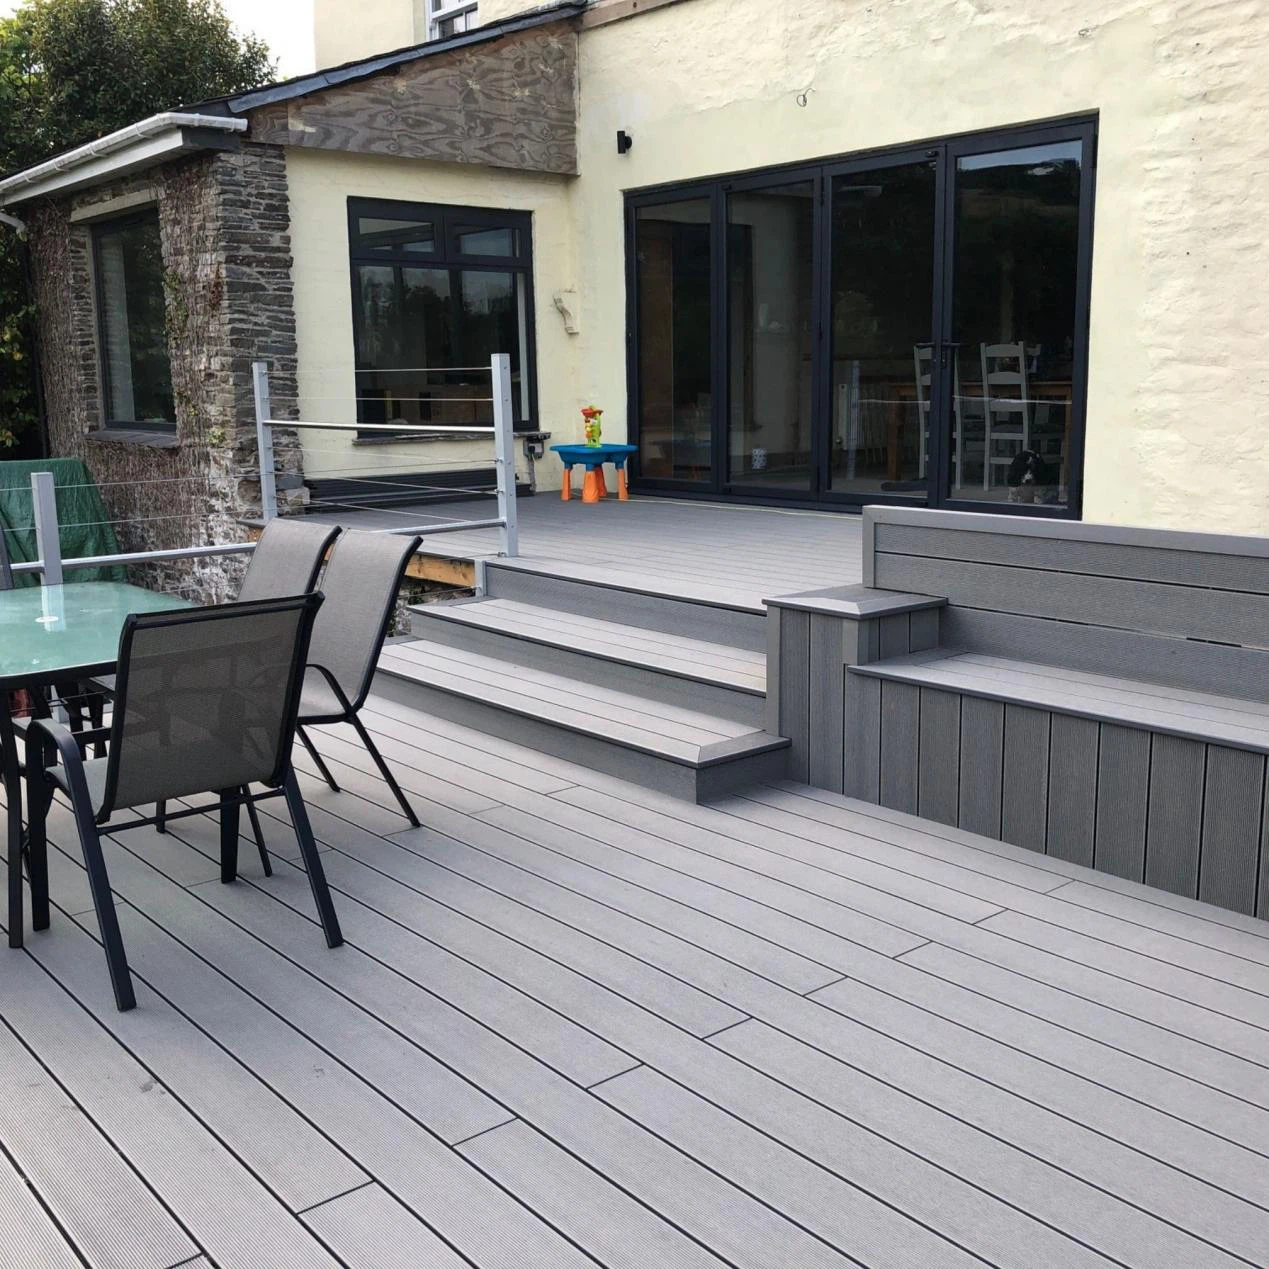
At Anhui Prairie Floor, we are deeply committed to sustainability. Not only do we use recycled raw materials in our structural formulations, but we also optimize closed-loop manufacturing processes to minimize carbon emissions and water usage. Our goal is to reduce natural forest depletion, contribute to global recycling networks, and cultivate a cleaner environment for future generations.
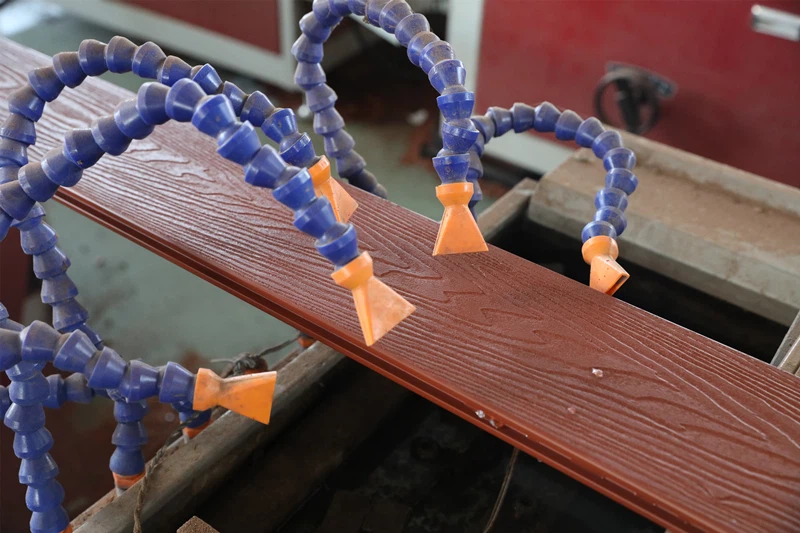
Every square meter of our functional antimicrobial flooring and WPC decking undergoes a 5-stage precision manufacturing process to guarantee dimensional stability, active pathogen defense, and high impact tolerance:
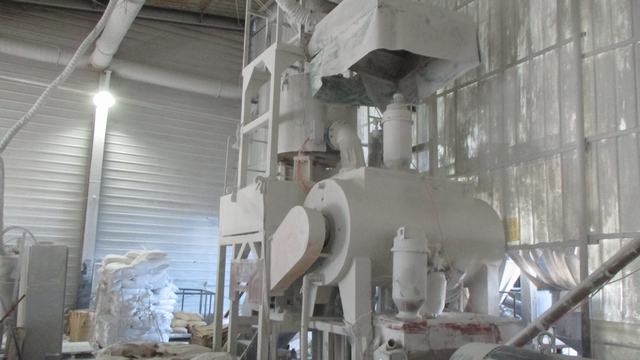
High-speed thermal compounding of polymers, bio-cork, plant fibers, and antimicrobial additives.
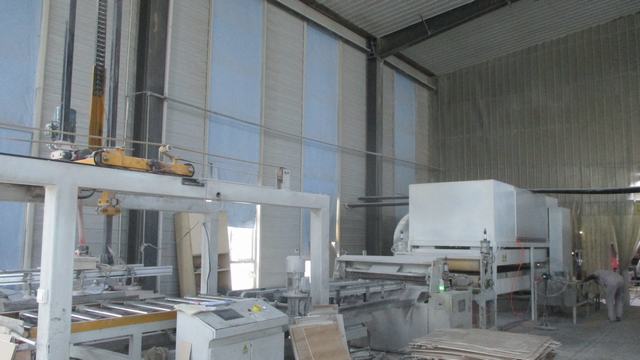
Dual-screw co-extrusion forming solid, dense, water-resistant core boards under high pressure.
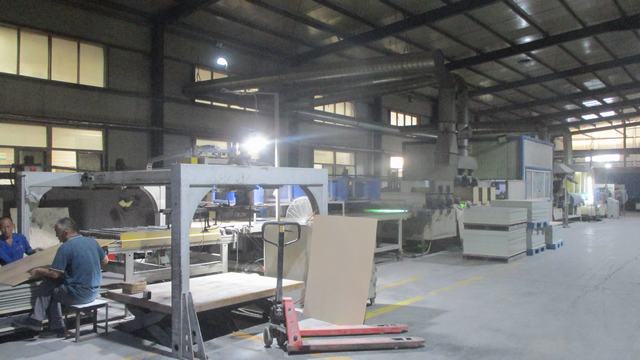
Curing top wear layers with UV radiation to lock in stain resistance and surface active biocides.
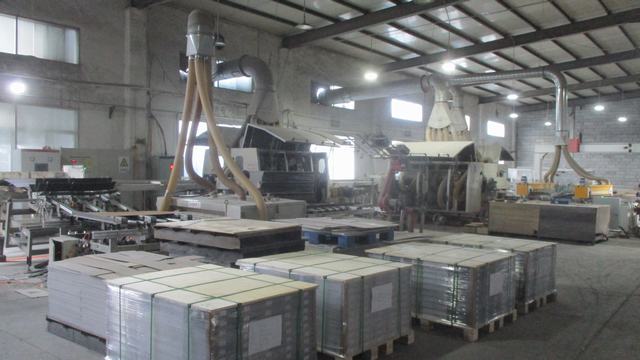
Precision CNC milling of click-lock, drop-lock, and tongue-and-groove joint profiles.
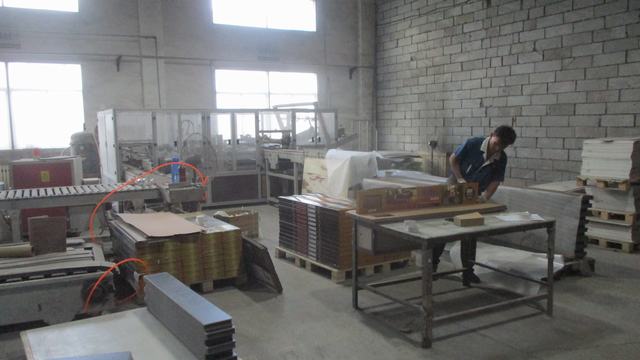
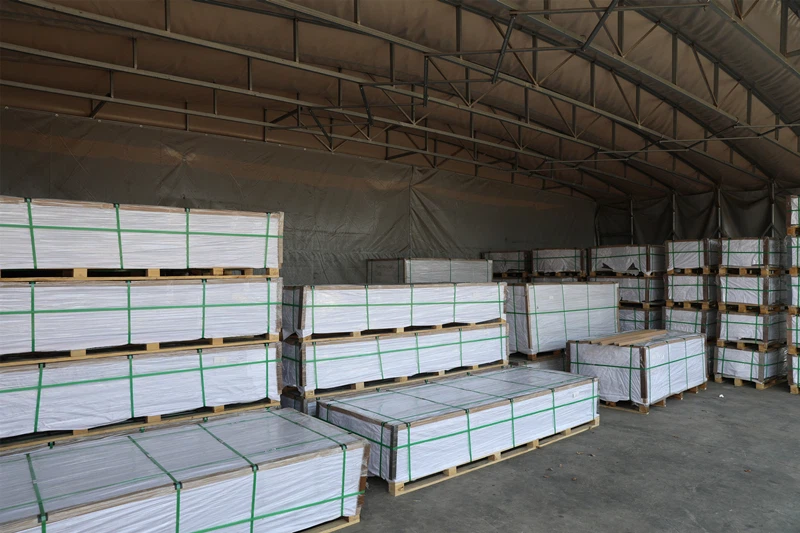
Automated quality inspection, protective film wrapping, and palletized export packaging.
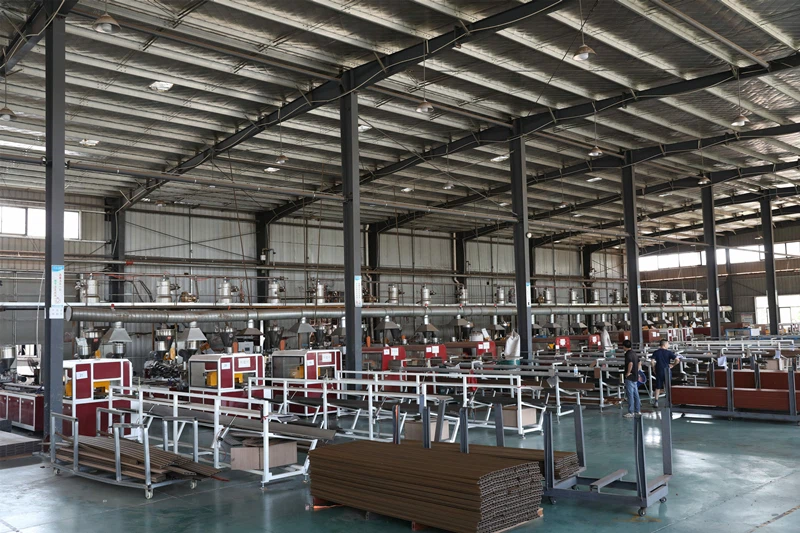
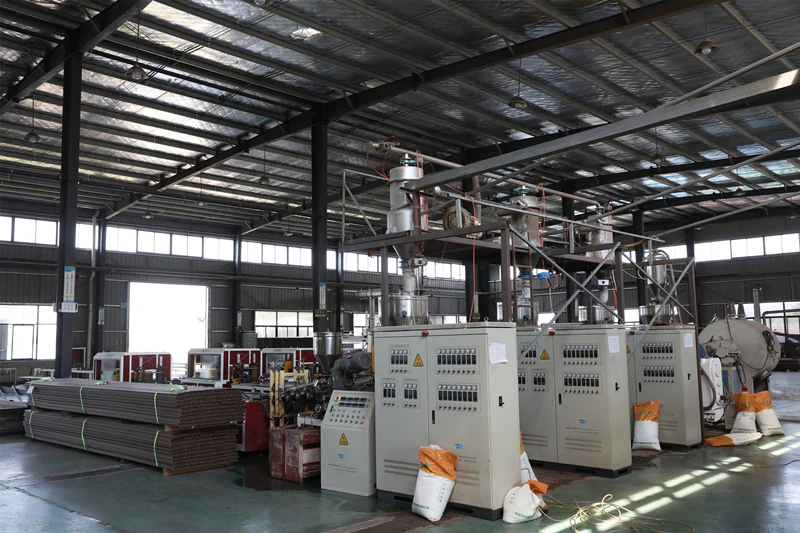
Antimicrobial surface coatings and specialized functional flooring products provide critical solutions across diverse high-demand sectors:
In sterile processing plants and vaccine production lines, micro-cracks and static accumulation create environments for microbial growth and electrostatic damage. Utilizing raised anti-static flooring systems combined with polyurethane wear coats guarantees both electrostatic discharge (ESD) safety and 24/7 bacterial suppression.
Hospitals require continuous protection against antibiotic-resistant bacteria like Methicillin-resistant Staphylococcus aureus (MRSA). Bio-passivated flooring surfaces eliminate pathogen footholds while enduring round-the-clock disinfections with harsh chemical agents.
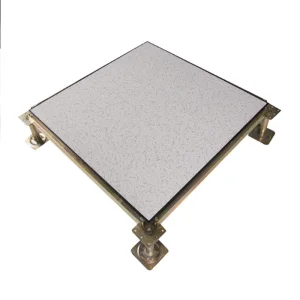
Data centers require static control combined with low-dust micro-environments. Encapsulated anti-static raised floor panels ($600 \times 600\text{ mm}$) provide structural load tolerance, air circulation, and dust-repellent antimicrobial surfaces to safeguard server hardware.
Heavy foot traffic in retail stores and schools accelerates mechanical wear. Low-VOC click-lock SPC laminate flooring equipped with antimicrobial surface treatments ensures healthy indoor air quality, scratch resistance, and low maintenance overhead.
When issuing RFQs or auditing international manufacturers for antimicrobial surfaces and specialized flooring, enterprise procurement managers should evaluate suppliers against five core criteria:
Explore the remainder of our engineered product suite, engineered to withstand extreme load dynamics, moisture intrusion, and micro-biological contamination.


If you are seeking innovative, eco-friendly, antibacterial, and high-durability flooring or surface coating solutions for commercial, medical, or industrial projects, contact our expert team today. We deliver custom formulation, material estimation, and global logistics support.
Anhui Prairie Floor Co., Ltd.: The perfect connection between nature and technology.
Request a Custom OEM Quote & Engineering Sample Kit Prairie Floor